
Industrial Burner Efficiency Ratings: What AFUE and Turndown Ratio Mean
When evaluating industrial burners, two ratings frequently dominate technical specifications: Annual Fuel Utilization Efficiency (AFUE) and turndown ratio. Understanding what these numbers mean is essential for selecting a burner that not only meets your process heat requirements but also minimizes fuel consumption and operational costs. For engineers, plant managers, and procurement professionals, AFUE and turndown ratio are not just abstract metrics—they directly influence energy bills, system reliability, and environmental compliance. This article explains both ratings in detail, explores their practical implications, and provides guidance on how to use them when selecting an industrial burner, with insights from industry specialist SHUXIN.
What Is AFUE and Why Does It Matter for Industrial Burners?
AFUE measures the percentage of fuel energy converted into usable heat over a typical heating season. In the industrial context, AFUE is calculated under standardized conditions and accounts for steady-state efficiency plus part-load losses. A burner with 85% AFUE means 85% of the fuel’s energy becomes heat; the remaining 15% escapes through flue gases, radiation, or other losses.
How AFUE Is Determined
Testing protocols vary by region, but generally AFUE considers:
- Combustion efficiency – the completeness of fuel burning
- Stack losses – heat carried away by exhaust gases
- Standby losses – heat lost when the burner is idle
High AFUE burners typically incorporate advanced heat exchangers, precise air-fuel ratio controls, and low-excess-air operation. However, AFUE alone does not tell the whole story—especially for industrial applications where the burner operates at varying loads.
Turndown Ratio: The Key to Flexible, Efficient Operation
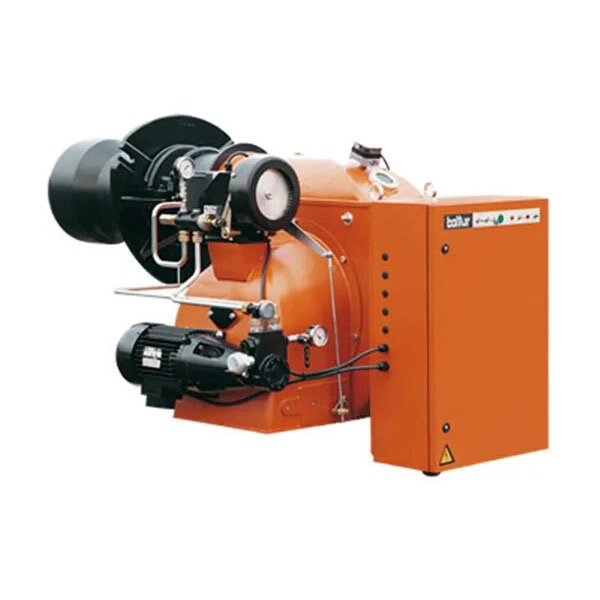
Turndown ratio (TDR) is the ratio between a burner’s maximum firing rate and its minimum stable firing rate. For example, a 10:1 turndown ratio means the burner can reduce its output to 10% of maximum capacity while maintaining stable combustion and acceptable efficiency.
Why High Turndown Matters
Industrial processes rarely run at constant heat demand. Batch operations, seasonal changes, and production line variations require the burner to modulate. A higher turndown ratio offers several advantages:
- Energy savings – avoids wasteful on/off cycling; the burner matches load precisely
- Reduced thermal stress – fewer cycles prolong equipment life
- Better temperature control – minimizes overshoot and undershoot
- Lower emissions – stable flame at low fire improves NOx and CO control
…
Click here for more detailed information on industrial burner efficiency ratings, specifically the meanings of AFUE and turndown ratio: https://www.sxburner.com/a/news/burner-efficiency-guide.html


