A Beginner’s Guide to CNC Glass Cutting Software

Entering the world of CNC glass cutting can feel overwhelming, especially when you are just starting to evaluate the software that controls the entire process. The right program does more than simply translate drawings into machine paths—it determines edge quality, cycle time, material yield, and even the safety of your operation. This guide is designed for beginners who need a clear, practical understanding of what CNC glass cutting software should do, how to evaluate it, and why an experienced partner like DISAI can make the difference between a frustrating trial-and-error period and a smooth, professional installation.

What Is CNC Glass Cutting Software?

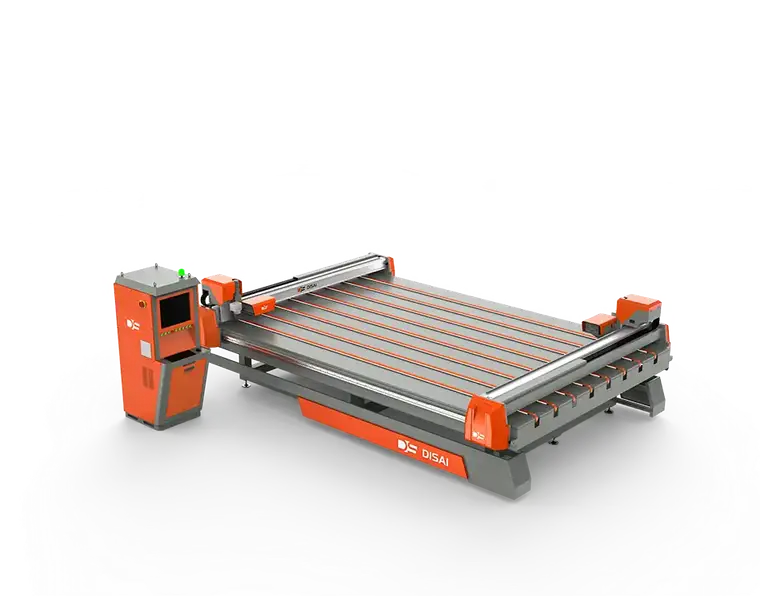
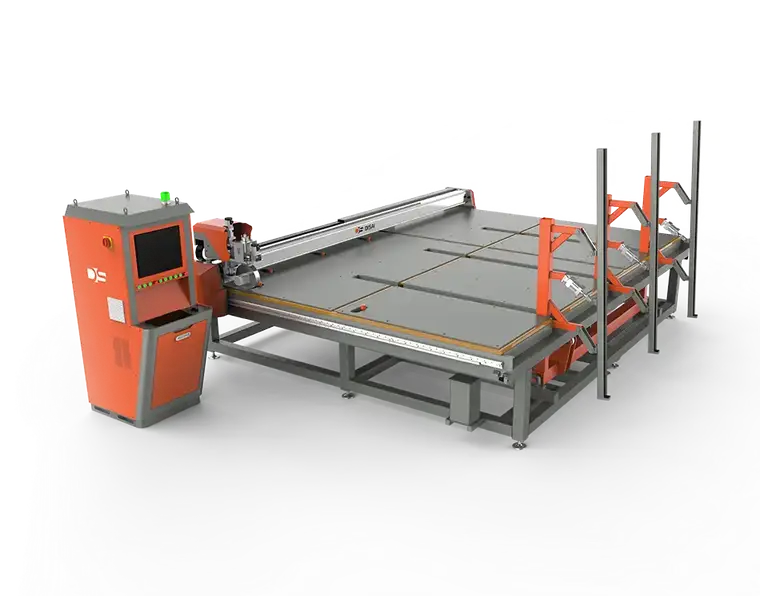
CNC glass cutting software is the digital brain of an automated glass cutting table. It takes geometric data from CAD files or custom shapes and generates optimized cutting paths for a machine equipped with a scoring head or a waterjet nozzle. Unlike generic CAM software, glass cutting programs must account for brittle material behavior, cutter pressure, wheel angle, and break-out considerations. For a beginner, understanding this distinction is critical—you are not just learning a generic drawing tool; you are engaging with a specialized application layer that directly affects glass breakage and edge quality.

Core Roles of the Software

  • Nesting: Arranging irregular shapes on a standard sheet to minimize waste and maximize yield.
  • Path Generation: Creating continuous, precise scoring lines with appropriate speed and pressure.
  • Machine Control: Sending commands to the servo drives, lift tables, and breaking systems.
  • Error Margins: Compensating for wheel wear, glass thickness variation, and temperature changes.

Key Features to Look for in Beginner-Friendly Software
Automatic Laser Marking Machine(Double Laser)

Not all software is created equal. Some are built for high-volume industrial operations, while others suit small workshops. As a beginner, you need a balance between capability and usability. The following features should be at the top of your checklist:

1. Intuitive Drawing and Import Tools

You should be able to import DXF/DWG files directly, or quickly draw simple rectangles, circles, and polygons within the software interface. Look for visual feedback, undo history, and snap functions that make design work forgiving.

2. Automatic Nesting with Manual Override

Automatic nesting saves time, but manual editing capability is equally important. You may need to prioritize a critical part or avoid a defect in the glass sheet. A flexible nesting engine lets you adjust rotation, spacing, and edge margins without fighting the program.

…

For more detailed information, please click to access the introductory guide to CNC glass-cutting software: https://www.disaiglass.com/industry-news/cnc-glass-guide/
Diamond vs Carbide Cutting Wheels: Which Wins?

Choosing between diamond and carbide cutting wheels is one of the most critical decisions in industrial fabrication, construction, and precision manufacturing. Install a diamond wheel where a carbide wheel belongs, and you risk thermal damage to the workpiece. Install carbide where diamond is needed, and production slows to a standstill. The two materials occupy fundamentally different positions in the cutting wheel spectrum — and understanding those positions is the difference between optimal throughput and costly trial-and-error. This guide breaks down the material science, real-world performance, and total cost implications to help you match the wheel to the job, with insights from DISAI’s years of manufacturing experience in industrial cutting tools.

Material Science: Why Diamond and Carbide Are Fundamentally Different

Before comparing performance, it is essential to understand what each wheel actually is. A diamond cutting wheel is not a blade made entirely of diamond; it is a steel core whose rim is embedded with industrial-grade synthetic diamond particles held in a metal, resin, or hybrid bond matrix. The exposed diamond particles act as the cutting tips. As the wheel spins, these particles fracture, chip, and abrade the workpiece at a microscopic scale.

A carbide cutting wheel, by contrast, is most commonly manufactured from tungsten carbide — a composite of tungsten and carbon atoms in a cobalt binder. It can be produced as a solid carbide disc or as a steel disc with carbide cutting inserts brazed onto the teeth. Carbide cuts by mechanical shearing, slicing, and chipping, relying on the sharpness and toughness of its edges rather than on abrasive erosion.

How Diamond Cuts: Abrasion at the Micro Level

Diamond is the hardest known natural material, rating a perfect 10 on the Mohs scale and cutting roughly four times harder than carbide. When a diamond wheel contacts concrete, brick, porcelain, or hardened steel, the diamond particles act like thousands of tiny chisels, micro-fracturing the surface and eroding material layer by layer. This abrasive mechanism gives diamond wheels an unrivaled ability to cut through materials that would destroy almost any other cutting edge.

How Carbide Cuts: Shearing with a Tough Edge

Tungsten carbide registers approximately 9 to 9.5 on the Mohs scale — extremely hard, but more importantly, it is exceptionally tough. Carbide absorbs impact, shock loads, and side pressure that would shatter diamond particles outright. When cutting softer materials such as aluminum, copper, plastics, and wood, carbide teeth shear through the material cleanly, producing a smooth finish without the friction and heat that diamond abrasion generates.

Diamond vs Carbide: The Core Performance Comparison

Automatic Laser Marking Machine(Double Laser)

To determine which wheel wins in a specific application, six parameters matter more than marketing claims:

  • Hardness: Diamond (Mohs 10) is roughly four times harder than carbide (Mohs 9 to 9.5), making diamond the practical choice for stone, concrete, and hardened alloys.
  • Cutting mechanism: Diamond cuts via abrasive micro-fracturing; carbide cuts via mechanical shearing and chipping.
  • Wear life: On hard materials such as concrete and masonry, diamond wheels typically outlast carbide wheels by 20 times or more before replacement is needed.

…

For more details on diamond cutting blades versus carbide cutting blades—and to find out which one comes out on top—please click here: https://www.disaiglass.com/industry-news/carbide-vs-diamond/

Cutting Tempered Glass: Myths vs Machine Reality

For decades, a single question has haunted glass fabricators, contractors, and DIY enthusiasts alike: Can tempered glass be cut? The answer, as with most things in materials engineering, is not a simple yes or no. Scattered across the internet are cautionary tales of exploding sheets, but also claims of miracle tools that can “score and snap” tempered glass with ease. The reality is far more structured. In this article, we separate what is myth from what modern machinery can genuinely achieve, and how companies like DISAI are redefining the limits of glass processing.

The Myth: Tempered Glass Can Be Scored and Snapped Like Standard Glass

One of the most persistent misconceptions is that tempered glass behaves like annealed glass when scored with a carbide cutter. The logic sounds reasonable: both are glass, both can be scratched, so why shouldn’t both break along a score line?

In practice, attempting to score and snap fully tempered glass results in near-instant fragmentation. The entire sheet bursts into the small, pebble-like pieces that tempering is designed to produce on impact. The reason lies in the very process that gives tempered glass its strength — a point we will examine in the next section.

The Physics Behind the Shatter: Internal Stress Is the Enemy of Cutting

Integrated Glass Cutting Table(Manual Loading)

Tempered glass is created by heating annealed glass to approximately 620°C, then rapidly cooling its surfaces with high-pressure air jets. This controlled thermal shock creates a state of differential stress: the exterior surfaces are in deep compression, while the interior core remains in tension. This stress balance is precisely what makes tempered glass approximately four to five times stronger than annealed glass of the same thickness.

However, this same stress balance is what makes post-tempering cutting impossible. When a cutting wheel penetrates the compressed surface layer, it creates a crack that immediately propagates through the tension zone. The stored energy releases explosively, and the glass shatters. It is not a matter of technique, tool quality, or operator skill — it is fundamental physics. No handheld tool, no amount of “specialized scoring,” can overcome this limitation.

Machine Reality: What Modern Technology Can Actually Achieve

If traditional cutting is physically impossible, what do we mean by “machine reality”? In professional glass processing, the answer is twofold: specialized high-pressure waterjet systems that sometimes work on tempered glass, and — far more commonly — CNC glass cutting systems that process glass before it enters the tempering furnace. Both approaches deserve careful examination.

…

For more detailed information on cutting tempered glass—including common misconceptions and the realities regarding machinery—please click here: https://www.disaiglass.com/industry-news/cutting-tempered/

Roller Bearing Cross Reference Guide for Buyers

A cross reference request usually arrives with a deadline attached: a line is down, a spare is out of stock, or an OEM quote came back at three times the budgeted price. The buyer is holding a bearing with a number stamped on the ring, or a number printed in a maintenance manual, and needs to know which other manufacturers’ bearings will drop into the same housing and carry the same load. This guide explains how roller bearing cross reference works at the data level, which dimensions and suffixes decide whether a substitution is safe, and what to send a supplier so the answer comes back correct the first time.

What a Cross Reference Can and Cannot Tell You

A cross reference is a mapping exercise. It takes one manufacturer’s designation and points to another manufacturer’s designation that shares the same boundary dimensions and bearing type. For the majority of standard radial bearings, that mapping is reliable because the dimensions themselves are standardized under ISO 15 for metric bearings and under ABMA inch-series standards for imperial sizes. A 25 mm bore ball bearing has a 25 mm bore regardless of whose logo is on the seal.

What a cross reference cannot tell you is whether two bearings are functionally identical. Cage material, internal clearance, precision class, sealing arrangement, heat treatment, and lubrication groove details are all outside the boundary-dimension standard. Two bearings can share a bore, outer diameter, and width and still behave very differently in a vibrating screen or a high-speed spindle. Treat every interchange table, including the ones published by major manufacturers, as a starting point for verification rather than a finished answer.

The Data You Need Before You Start

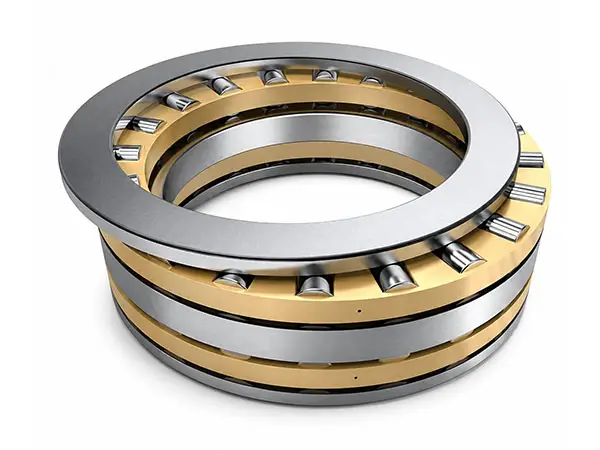
Cylindrical Roller Thrust Bearings

Most failed cross reference attempts fail at the input stage. A partial part number produces a partial answer. Before contacting anyone, collect the following:

  • The complete designation, including every prefix and suffix, copied exactly as printed on the bearing or in the manual.
  • Bore diameter, outer diameter, and width, measured with a caliper if the markings are worn.
  • Bearing type: cylindrical roller, spherical roller, tapered roller, needle roller, or ball.
  • Operating conditions: rotational speed, radial and axial load, temperature range, and lubrication method.
  • Shaft and housing fit, and whether the outer ring is located by a shoulder, a snap ring, or a housing cover.

Read the whole designation, not the first four digits

The basic number identifies the size series and bore. Everything after it modifies the bearing. A 22216 and a 22216 E are the same envelope but may differ in internal design and load rating. A 22312 EK has a tapered bore; a 22312 E does not. If you drop the suffix when searching, you will get results that physically fit and then fail early.

…

For more detailed information regarding the comparison chart for roller bearing buyers, please click here: https://www.chgbearingtech.com/blog/roller-bearing-cross-reference-guide/

Metric vs Inch Roller Bearings: What to Know

Selecting a roller bearing looks straightforward until the dimensions you need do not exist in the system you assumed. A shaft measuring 2.4375 inches, a housing bored to 110 mm, or a legacy drawing dated 1974 can each point to a bearing that is stocked in one measurement system and simply unavailable in the other. Metric and inch roller bearings are not interchangeable through conversion alone: they follow different standards, different tolerance philosophies, and different supply chains. Getting the distinction right at the specification stage prevents redesign, rework, and unplanned downtime. This guide explains how the two systems differ, where they appear to overlap, and how to specify and source the correct bearing for your application.

The Fundamental Difference Between Metric and Inch Roller Bearings

Metric roller bearings are dimensioned according to ISO boundary dimension standards, with bore, outside diameter, and width expressed in millimeters. Inch roller bearings follow ABMA and ANSI conventions, with boundary dimensions expressed in inches, including fractional bores such as 1 7/16″, 2 3/16″, and 3 15/16″. The two families exist because North American industry standardized on inch dimensions long before metrication spread through global manufacturing, and much of that installed base is still running today.

The critical point for anyone specifying a bearing is this: converting millimeters to inches does not produce an inch bearing. A 25 mm bore is 0.9843 inches, not 1.000 inch. A 50 mm bore is 1.9685 inches, not 2.000 inches. Even where two bearings land within a few thousandths of an inch of each other in envelope dimensions, the internal geometry, cage design, corner radii, and tolerance zones are defined separately, so they are not drop-in replacements.

Why the Numbers Never Line Up Exactly

Metric bore sizes progress in clean increments: 20, 25, 30, 35, 40 mm, and so on. Inch bore sizes generally progress in fractional increments, frequently sixteenths of an inch. Because one inch equals 25.4 mm, the two sequences only coincide at rare points. This is why a bearing that looks like a near match on a drawing often will not seat correctly on the shaft or in the housing.

Standards Bodies and Designation Systems

Metric bearings are governed by ISO standards, with designation systems built around series numbers that describe the internal design and width series. Inch bearings are governed by ABMA and ANSI standards, and their designations often read very differently, sometimes using prefix letters or numeric series that have no metric equivalent. When you cross-reference between the two systems, you are not translating a part number; you are identifying a functionally similar bearing and then verifying that it fits, carries the load, and survives the operating conditions.

Tolerances, Fits, and Load Ratings

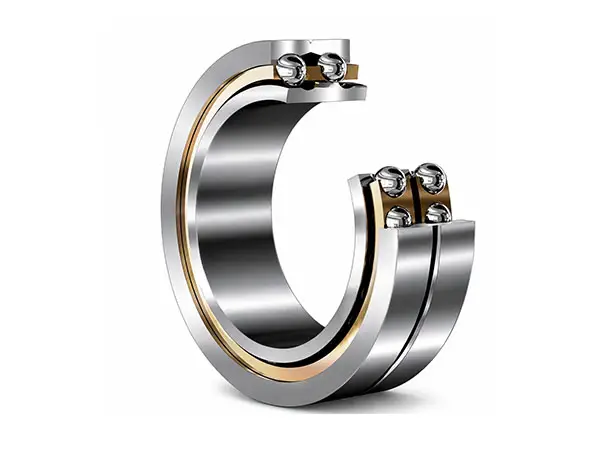
Double Row Angular Contact Ball Bearings

Dimension is only one layer of the difference. Tolerance is the one that causes the most expensive mistakes.

Metric bearings use tolerance classes such as P0, P6, P5, and P4, with bore and outside diameter tolerances typically expressed as symmetric plus and minus values in micrometers. Inch bearings historically use tolerance classes defined by ABMA, where bore tolerances may be expressed in ten-thousandths of an inch and follow different conventions, including unidirectional tolerance zones in certain classes. A shaft that fits a metric bearing perfectly may be marginally too tight or too loose for an inch bearing of nominally similar size.

Internal clearance follows the same pattern. Metric clearances are specified in micrometers; inch clearances are traditionally specified in ten-thousandths of an inch. The specified ranges for comparable applications are not always mathematically equivalent once converted, so clearance should be treated as a separate specification decision rather than a unit conversion.

…

For more details regarding metric and imperial roller bearings—including everything you need to know—please click here: https://www.chgbearingtech.com/blog/metric-vs-inch/

High-Speed Roller Bearings: Design Limits Explained

Roller bearings carry heavier loads than ball bearings of the same envelope, but that advantage comes with a speed penalty. As rotational speed rises, rollers gain centrifugal force, internal load paths shift, and the heat generated inside the bearing begins to outrun the heat it can shed. At some point the bearing stops behaving like a load-carrying component and starts behaving like a thermal and dynamic problem. Knowing where that point sits, and which design variables move it, is what separates a reliable high-speed arrangement from one that fails early. This article explains the physical limits behind roller bearing speed ratings and the design decisions that raise them.

What a Speed Rating Really Tells You

Bearing catalogs publish two different numbers, and confusing them is one of the most common specification errors. The limiting speed is a catalog-level ceiling for a given bearing under defined reference conditions, typically light load, correct lubrication, and adequate heat dissipation. The thermal reference speed, defined in ISO 15312, is derived from a heat balance: the speed at which heat generation inside the bearing equals heat dissipation through a defined housing and shaft, for a stated reference temperature rise.

Neither figure is a guarantee. Both assume favorable conditions that a real application rarely reproduces exactly. A roller bearing rated at one speed in a catalog may run far below that rating inside a poorly cooled, heavily preloaded housing, or comfortably above it when oil-jet lubrication and a rigid, thermally stable shaft are in place.

The Physical Limits Behind the Numbers

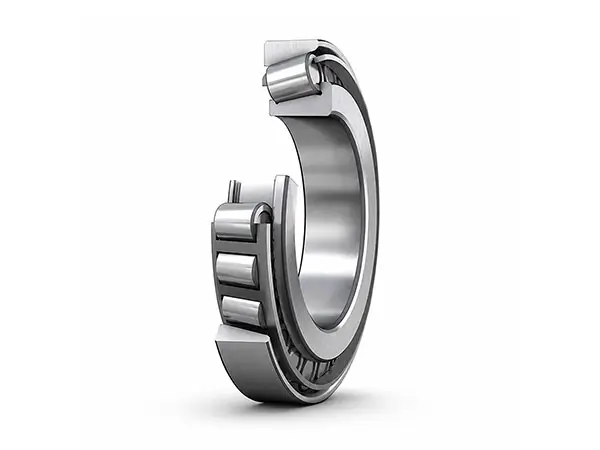
Single Row Tapered Roller Bearings

Heat generation versus heat dissipation

Every high-speed bearing is a heat engine in a losing battle with itself. Friction torque comes from rolling resistance, sliding in the contacts, lubricant churning, and cage interaction. That heat must travel out through the rollers, rings, shaft, and housing. As speed climbs, heat generation rises faster than most conduction paths can carry heat away, and the lubricant film that keeps metal off metal thins as temperature increases.

The practical result is a runaway threshold. Beyond a certain speed, each increment of friction produces more heat, which reduces film thickness, which increases friction. Once that loop begins, bearing life collapses quickly. This is why temperature, not rotational speed, is usually the true limiting variable.

Centrifugal and gyroscopic effects on the rollers

A cylindrical or tapered roller orbiting a shaft at high speed experiences centrifugal force proportional to the square of rotational speed. At moderate speeds this force is negligible. At high speeds it presses the roller against the outer raceway, alters the load distribution around the bearing, and can cause the roller to skew within its pocket. For spherical and tapered rollers, the effect is more pronounced because of greater mass and more complex geometry.

The consequence is a bearing that carries its rated load at low speed but loses effective capacity as speed rises. Nothing about the steel has changed; the internal load path has.

…

For more detailed information on high-speed roller bearings—including an in-depth look at design limits—please click here: https://www.chgbearingtech.com/blog/roller-bearing-rpm/

Radial vs Axial Load Capacity in Roller Bearings

Roller bearings rarely fail because someone picked the wrong catalog number. They fail because the load direction was misunderstood. A bearing that handles a heavy radial load with ease can be destroyed surprisingly fast by a modest axial thrust, and the reverse is equally true. Engineers comparing radial versus axial load capacity in roller bearings are usually trying to answer one practical question: which rolling element geometry matches the forces in my application, and how much of each direction can it realistically carry? The answer depends on contact angle, raceway geometry, roller length-to-diameter ratio, and how the load is distributed across the loaded zone. This guide breaks down the mechanics, compares the major roller bearing families, and explains how to read load ratings before committing to a design.

Radial and Axial Loads: Two Directions, Two Different Mechanisms

The distinction sounds trivial until you look at how the rolling elements actually react. A radial load pushes the shaft perpendicular to its centerline, while an axial load pushes it along the centerline. Those two force vectors engage completely different parts of the bearing’s internal geometry.

How radial loads travel through a roller bearing

Under a purely radial load, roughly half the rollers in a typical bearing carry the load, forming a load zone that spans about 180 degrees of the raceway circumference. Each loaded roller deforms slightly against both rings, and the resulting contact stress is spread along the full roller length. Because cylindrical rollers make line contact rather than point contact, the load is distributed across a much larger area than in a ball bearing of similar size. That is the fundamental reason roller bearings achieve high radial capacity in a compact envelope.

How axial loads travel through a roller bearing

An axial load cannot simply be pressed into a cylindrical raceway. It has to be redirected by geometry. There are only two ways to do this: build a contact angle into the bearing so the roller axis is tilted relative to the shaft axis, or use flanges and thrust shoulders that guide the roller ends. In a tapered roller bearing, the contact angle converts part of the axial thrust into a radial reaction at the cone back face and cup face. In a cylindrical roller bearing with a fixed rib, the axial load is taken by sliding contact between the roller end face and the rib, which is a fundamentally different and far more limited load path.

Combined loads are the normal case

Pure radial or pure axial loading is mostly a textbook simplification. Gear drives, pulley arrangements, and inclined shafts all produce combined loading with a moment component. In these situations the bearing is evaluated against an equivalent dynamic load that weights the radial and axial components according to the bearing’s X and Y factors, and against an equivalent static load for peak or shock conditions. The X and Y factors come from the bearing manufacturer and vary with the ratio of axial to radial load and with the contact angle.

Which Roller Bearing Type Handles Which Load Direction

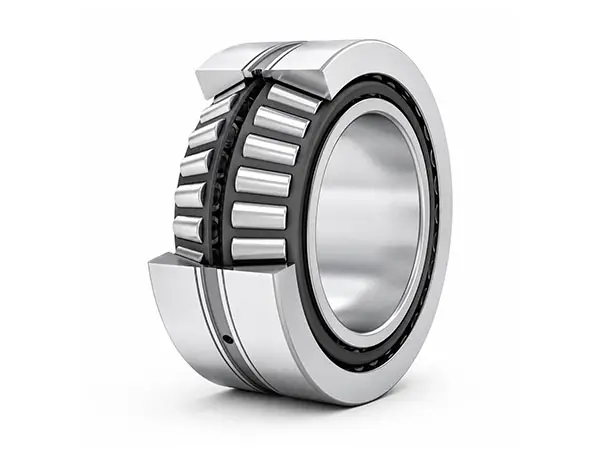
Double Row Tapered Roller Bearings

Roller bearing families are not interchangeable when thrust is present. The table below summarizes how each type behaves, followed by the practical consequences.

  • Cylindrical roller bearings (NU, NJ, NUP, N designs): Very high radial capacity, essentially zero axial capacity in the basic NU/N design. NJ and NUP variants with ribs accept limited axial loads in one or both directions, but only at low to moderate levels and with careful attention to lubrication of the rib contact.
  • Tapered roller bearings: High radial capacity combined with substantial axial capacity in one direction per bearing. Mounted in pairs or opposed arrangements they take thrust in both directions. The induced axial force generated by the contact angle must be accounted for in the arrangement calculation.

…

For more detailed information regarding the radial and axial load-carrying capacities of roller bearings, please click here: https://www.chgbearingtech.com/blog/radial-axial-load/

Best Seals for Roller Bearings in Dusty Environments

Dust is not a nuisance for roller bearings — it is a wear mechanism. In mining, cement, aggregate, agricultural and steel plants, airborne particles smaller than a grain of sand enter bearing housings, mix with grease, and turn a smooth raceway into an abrasive grinding surface. The seal is the only barrier between that environment and the rolling elements, which is why seal choice often matters more than bearing brand in dusty applications. This guide compares the seal types commonly fitted to roller bearings, explains where each one works and where it fails, and sets out the selection criteria that keep equipment running between planned shutdowns.

Why the Seal, Not the Bearing, Decides Service Life in Dust

A roller bearing running in a clean, well-lubricated housing can reach its calculated L10 life without difficulty. The same bearing in a quarry conveyor or a cement kiln fan rarely gets there. In practice, most premature roller bearing failures in dusty plants trace back to contamination rather than fatigue.

The damage sequence is predictable:

  • Fine particles pass the seal and enter the grease cavity.
  • Particles migrate into the raceway contact zone and act as an abrasive third body.
  • Surface roughness increases, film thickness collapses, and local stress risers form.
  • Spalling, cage wear and overheating follow, often within a fraction of the expected service life.

Particle size determines how much damage a given ingress rate causes. Particles in the 5 to 20 micron range are the most destructive for roller bearings, because they are small enough to enter the contact ellipse but large enough to bridge the lubricating film. Coarse grit tends to be blocked by almost any seal; it is the respirable fraction that a seal must be designed to stop.

The Main Seal Types Used on Roller Bearings

Four-Row Cylindrical Roller Bearings

There is no universal best seal. Each design trades sealing efficiency against friction, speed capability, tolerance to misalignment and cost. Understanding those trade-offs is what allows a maintenance engineer to specify the right barrier for a specific machine.

Contact Lip Seals

Elastomer lip seals — typically nitrile rubber (NBR), hydrogenated nitrile (HNBR) or fluoroelastomer (FKM) — press a flexible lip against a ground shaft or wear sleeve. They offer the lowest leakage and the best exclusion of fine dust among single-element seals, which is why they remain the default on plummer block housings, gearbox shafts and many mounted bearing units.

…

For more details on the best seals for roller bearings in dusty environments, please click here: https://www.chgbearingtech.com/blog/best-seals-for-roller-bearings-in-dusty-environments/

Galvanized vs Painted Steel Structure Warehouse

The fastest way to make costly mistakes in a steel warehouse project is to rely only on price and looks. We’ve seen it ourselves—what matters in the end is which protection system can reliably safeguard your investment against corrosion, downtime, and hidden maintenance costs.

When comparing galvanized and painted steel structure warehouses, the main differences are in how each system prevents corrosion and how that affects your maintenance needs, safety, appearance, and the total cost over time.

After years working with steel structures in all types of environments, we’ve learned that appearances can be misleading. A painted warehouse might look fresh and impressive at first. But without the right anti-corrosion plan, it can turn into an expensive headache. Galvanized steel costs more at the start but shows its value when the weather or chemicals start to attack. Let’s dive into the real differences and what we’ve seen in actual projects.

What’ s the real difference between galvanized and painted warehouse steel?

Galvanized and painted steel both use the same base material, but their protection strategies change everything. Galvanized steel is coated in zinc, usually by hot-dip galvanizing, which acts as a physical barrier and even sacrifices itself to protect the steel beneath if scratched. Painted systems use multiple layers—primer, intermediate paint, and topcoat—primarily to block moisture and corrosion, but their effectiveness depends heavily on how well the paint is applied.

In our own factory, we see that galvanizing is far more reliable for warehouses exposed to harsh conditions—coastal air, fertilizer dust, chemical vapors, or high humidity. Painted steel is better when we want flexibility in color, when members are too big for the galvanizing tanks, or when the whole project needs to move quickly with lower startup costs. But we always tell customers: painted steel is only as good as the coating job and ongoing maintenance.

…
Click here for more details on Galvanized vs Painted Steel Structure Warehouse:https://www.lydoer.com/news/galvanized-vs-painted-steel-structure-warehouse.html

Measurable Benefits of Proper Vibrating Screen Tensioning

Proper tensioning of vibrating screen mesh is often underestimated in its impact on overall screening performance. Yet, for operations handling bulk materials—from aggregate to minerals—the tension applied to the screen cloth directly determines throughput accuracy, wear life, and operating costs. When tension is too loose, the screen flexes excessively, leading to premature fatigue, blinding, and inefficient particle separation. When over-tightened, the mesh may crack or distort, reducing screening area. In either case, measurable losses occur. This article examines the quantitative advantages of maintaining correct screen tension, drawing on field data and engineering principles, and explains how Haiside tensioning systems help operators achieve consistent, verifiable results.

1. The Direct Impact on Screening Efficiency and Throughput

The primary function of a vibrating screen is to separate particles by size. Screen tension plays a critical role in how effectively the mesh transmits vibration to the material bed. A properly tensioned screen maintains a uniform amplitude across its surface, ensuring that each particle receives the same acceleration and stratification force.

Quantifying Particle Separation Accuracy

Studies have shown that a tension deviation of just 10% from optimal can reduce screening efficiency by 15–20%. Loose screens allow the mesh to flutter independently of the screen deck, creating localized areas of reduced vibration. Oversized particles may pass through momentarily stretched openings, while near-size particles become trapped, increasing pegging. Conversely, a properly tensioned screen from Haiside maintains consistent opening dimensions, resulting in tighter cut-point control. In a typical 2-deck operation, proper tension can improve oversize recovery by 8–12% and reduce misplaced fines in oversize product.

How Tension Affects Material Flow Rate

Throughput is directly linked to the open area available for material passage. When a screen is loose, it bows under the load, reducing the effective screening surface. Over multiple cycles, this bowing increases, further restricting flow. Proper tensioning ensures the mesh remains flat and taut, maximizing open area. Field measurements indicate that restoring correct tension can increase mass flow by 6–10% on the same screen deck without changing stroke or speed. For a plant processing 500 tons per hour, this translates to an additional 30–50 tons per hour of correctly sized product.

2. Extended Screen Life – Reducing Replacement Frequency

Cooperation Customer

Screen cloth is a consumable with significant cost implications. Many operators accept a short life as normal, but the failure mode is often linked to improper tension rather than inherent wear. A screen that is too loose undergoes repeated flexing at the tensioning hooks and around the support bars. This cyclic bending stress causes fatigue cracks that propagate quickly, leading to sudden failure.

…

Click here for more details on the measurable benefits of proper vibrating screen tensioning: https://www.hsd-industry.com/news/measurable-benefits-of-proper-vibrating-screen-tensioning/